Quality
Quality & Inspection
How every pressed steel radiator is inspected and pressure-tested before it leaves our factory.
Quality Philosophy
Our Approach to Quality
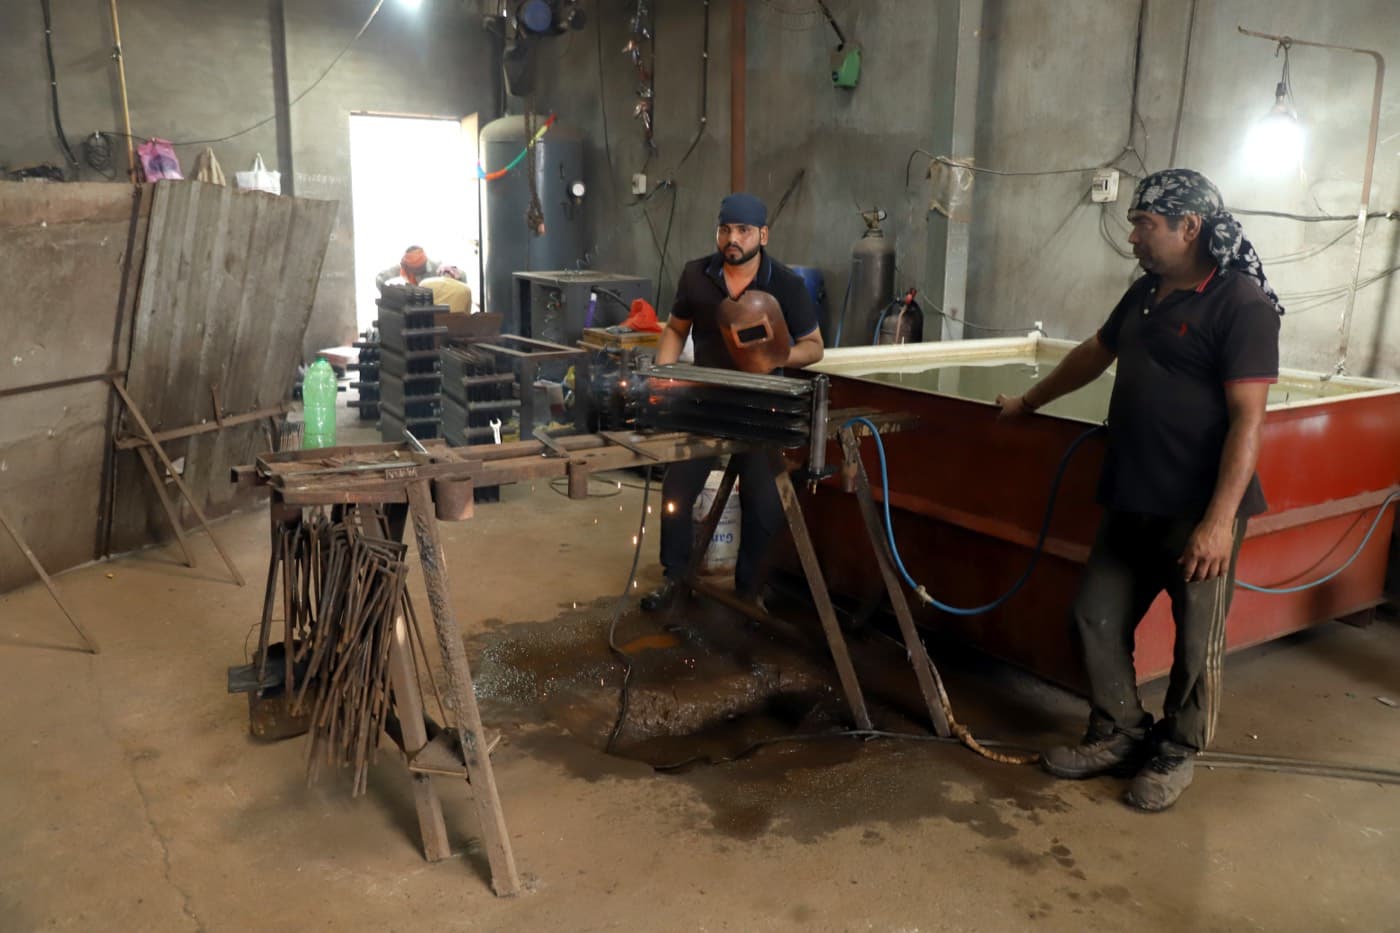
Every pressed steel radiator we build is pressure-tested with air and oil at 2.5 kg/cm² — well above the 2 kg/cm² maximum operating pressure it is rated for — before it is finished and dispatched. Panels, welds and flanges are checked at each stage of assembly rather than only at the end, so faults are caught before a unit reaches the paint line.
Inspection
Inspection Process
Every radiator passes through these checks on our factory floor before it is approved for dispatch.
Material Inspection
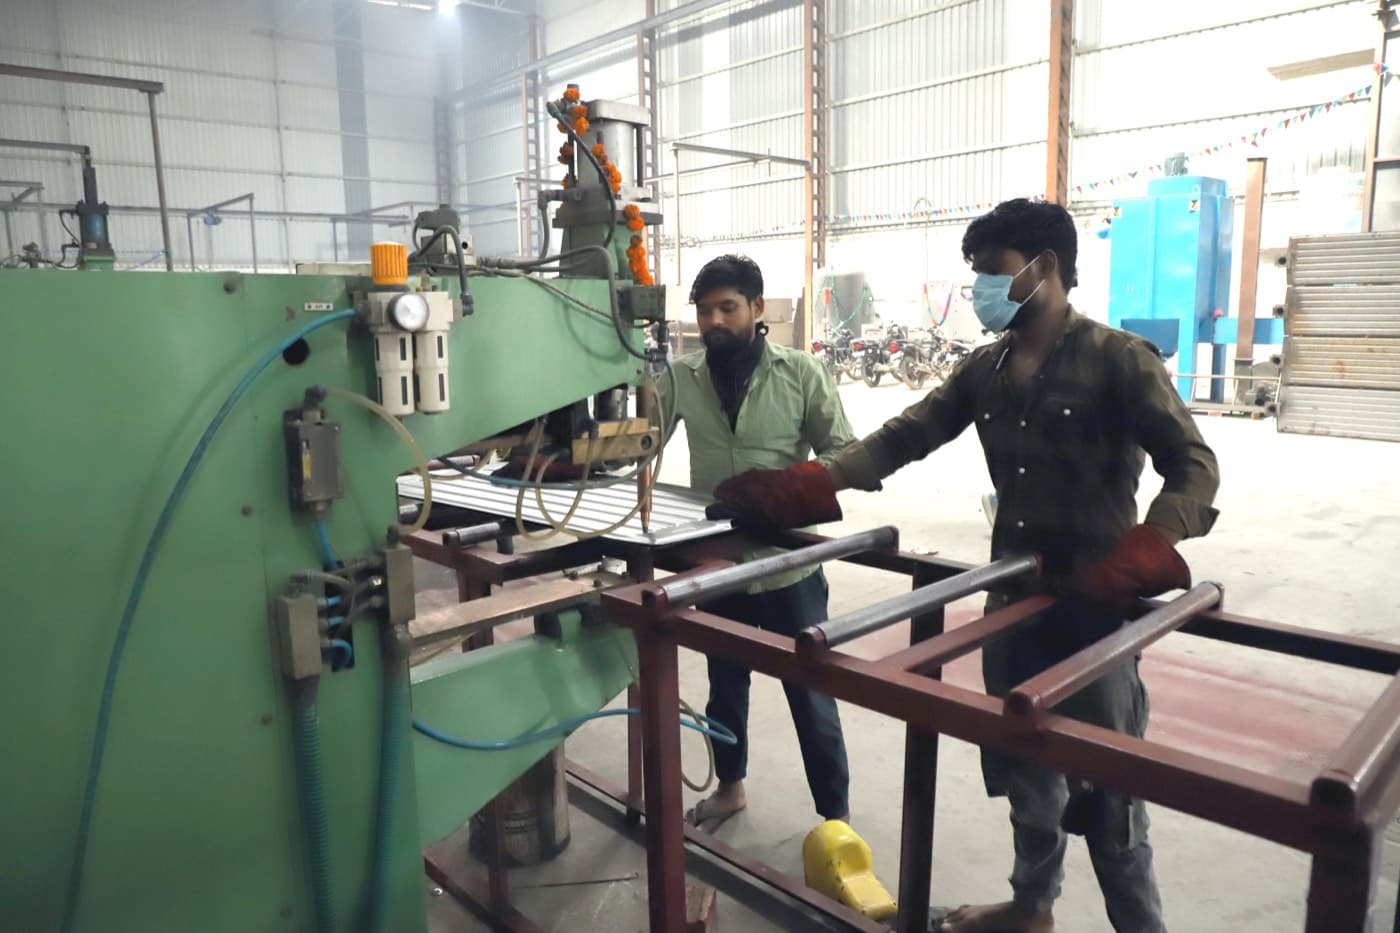
Incoming CRCA sheet and header pipe are checked before being released to the forming line.
Dimensional Inspection
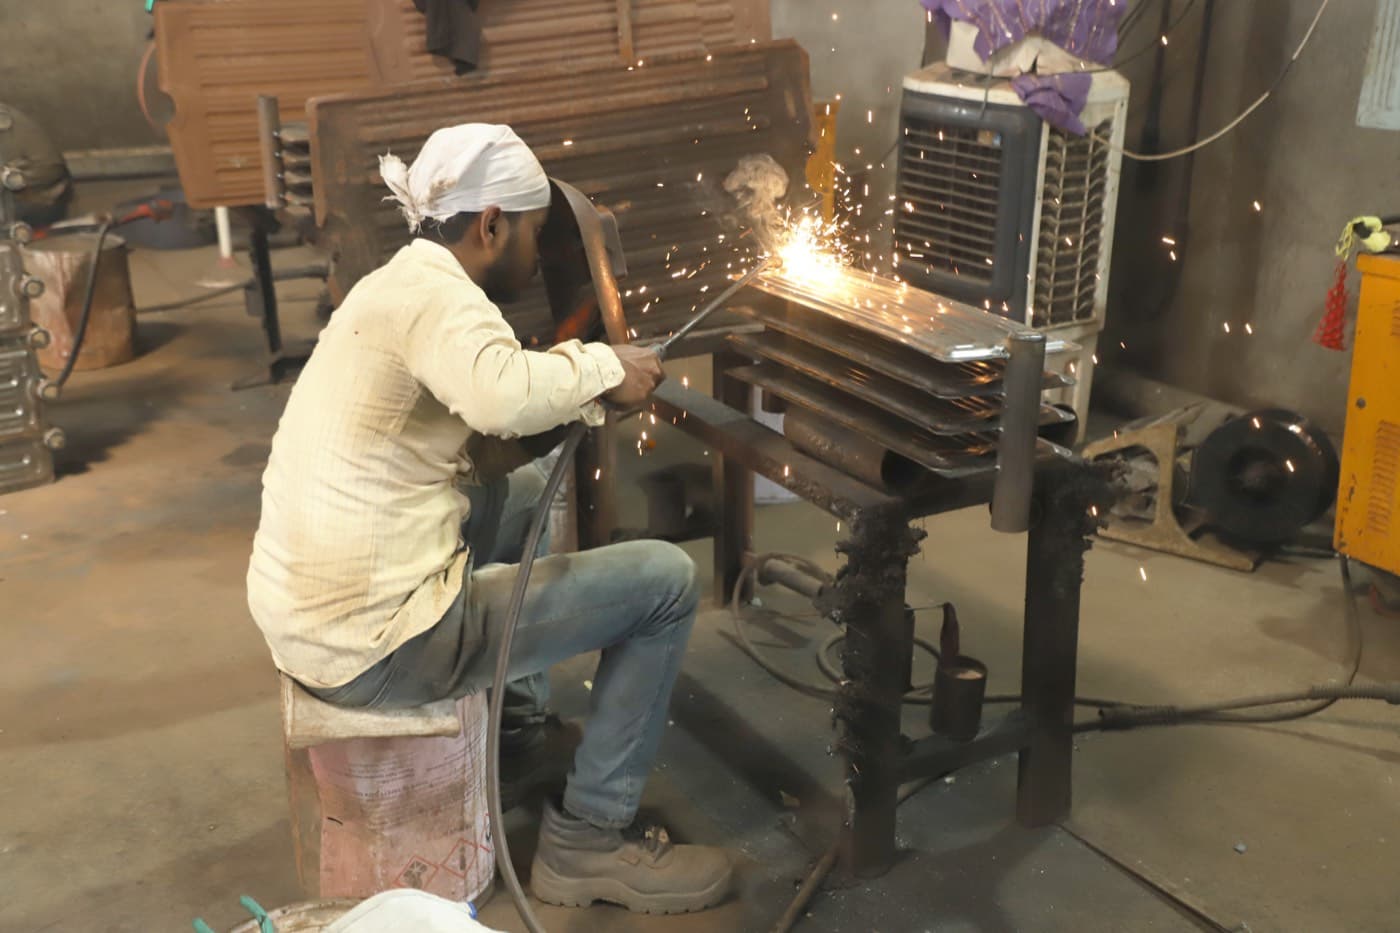
Formed panels and headers are checked against the order drawing for panel size, OD and header length.
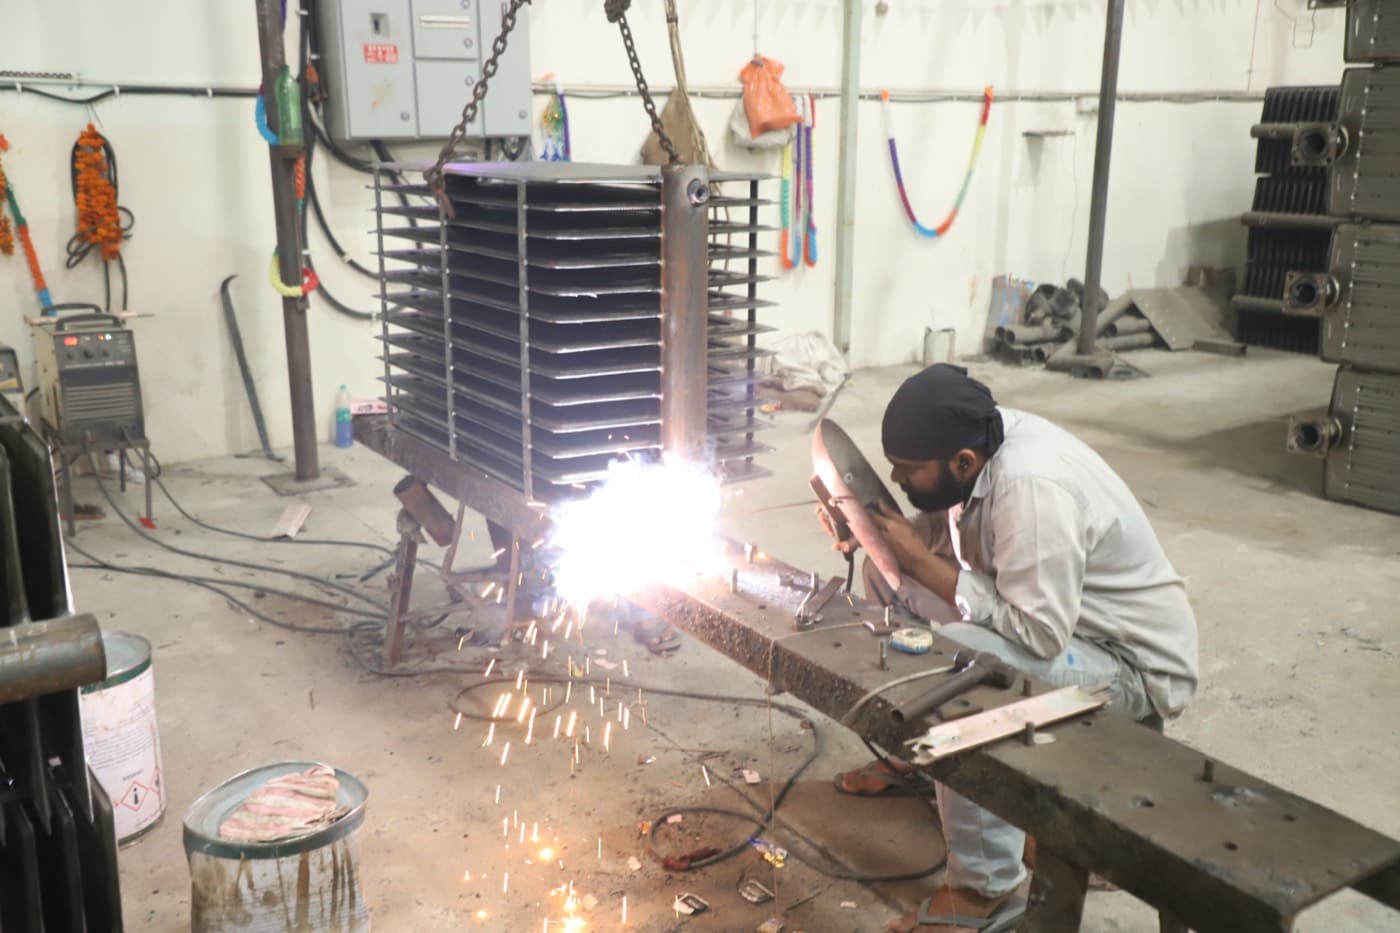
Welding Inspection
Panel-to-header and assembly welds are visually inspected for seam consistency before a unit proceeds to testing.
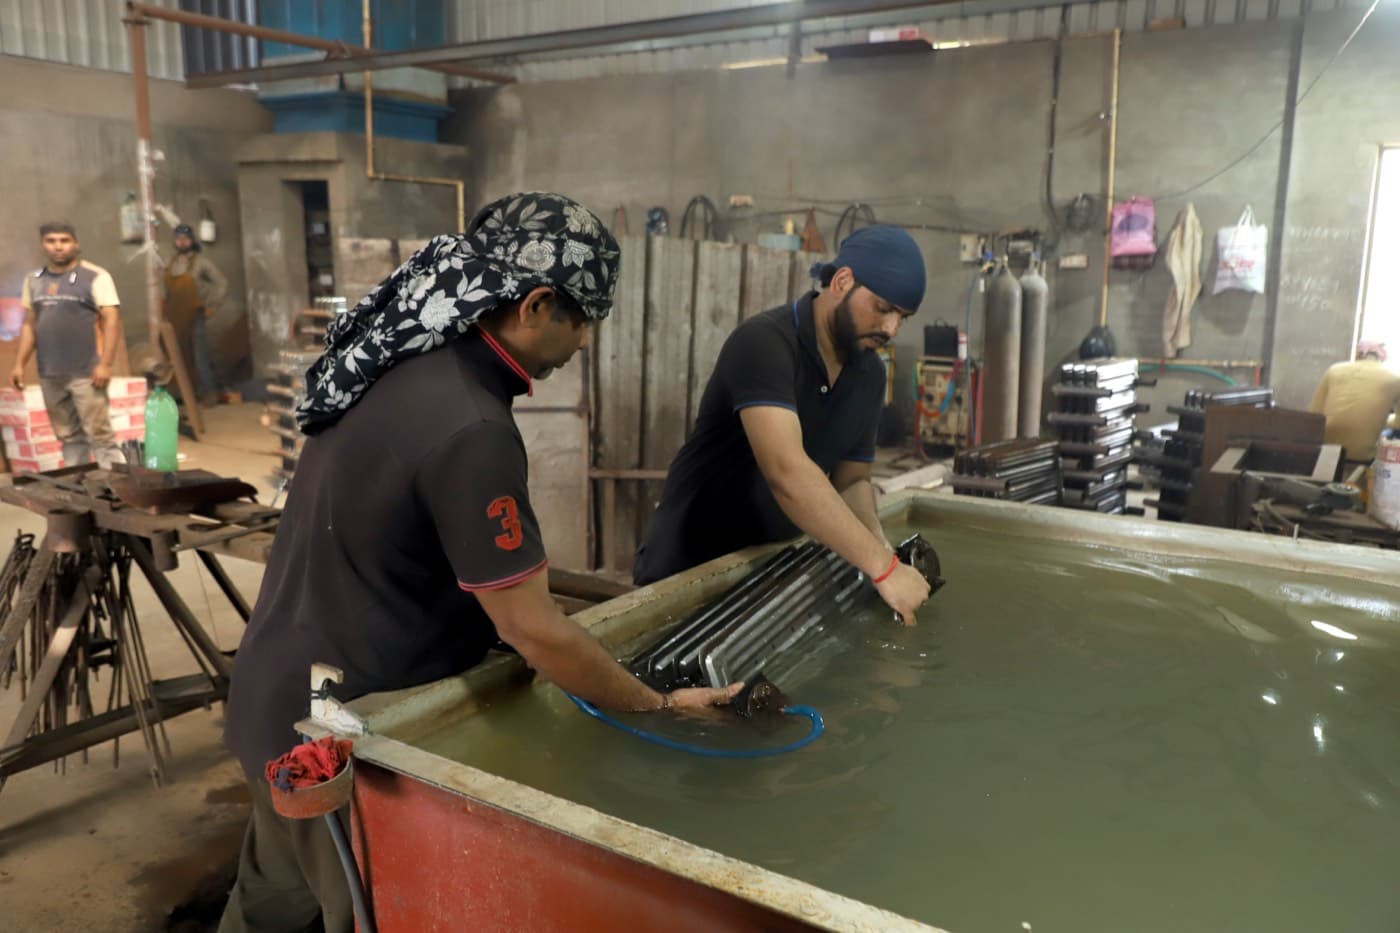
Leak / Pressure Testing
Each radiator is submerged in the test tank and pressurized with air and oil to 2.5 kg/cm² to confirm every seam holds under pressure.
Final Inspection
Painted, finished units are given a final visual check for surface finish and completeness before packing. See the Manufacturing page for packaging and dispatch details.
Certifications
Certifications & Standards
Formal certifications are not yet listed — our quality process is built around pressure-testing every unit at 2.5 kg/cm² before dispatch. Contact us for test documentation on a specific order.
Have Testing or Certification Requirements?
Share your specification and required standards with our team for confirmation.