Manufacturing
Manufacturing Capabilities
Inside our 2,800 sq. ft. factory in Jaipur — from raw sheet steel to a tested, painted radiator.
Factory Overview
Our Manufacturing Facility
Shree Shyam Enterprises operates a 2,800 sq. ft. manufacturing unit in the Sarna Dungar Industrial Area, Jaipur, with a team of around 90 people, including a dedicated 4-member quality and engineering team. The facility runs its own panel-forming, welding, leak/pressure-testing and painting lines, so a radiator moves from raw sheet to a tested, painted, dispatch-ready unit without leaving the premises.
Capacity
Manufacturing Capacity
Process
Manufacturing Process
Our nine-stage production flow, from raw steel to a packed, dispatch-ready radiator.
- 01
Raw Material
Cold-rolled low-carbon steel (CRCA) sheet and mild-steel pipe are received and staged for panel pressing and header fabrication.
- 02
Cutting / Forming
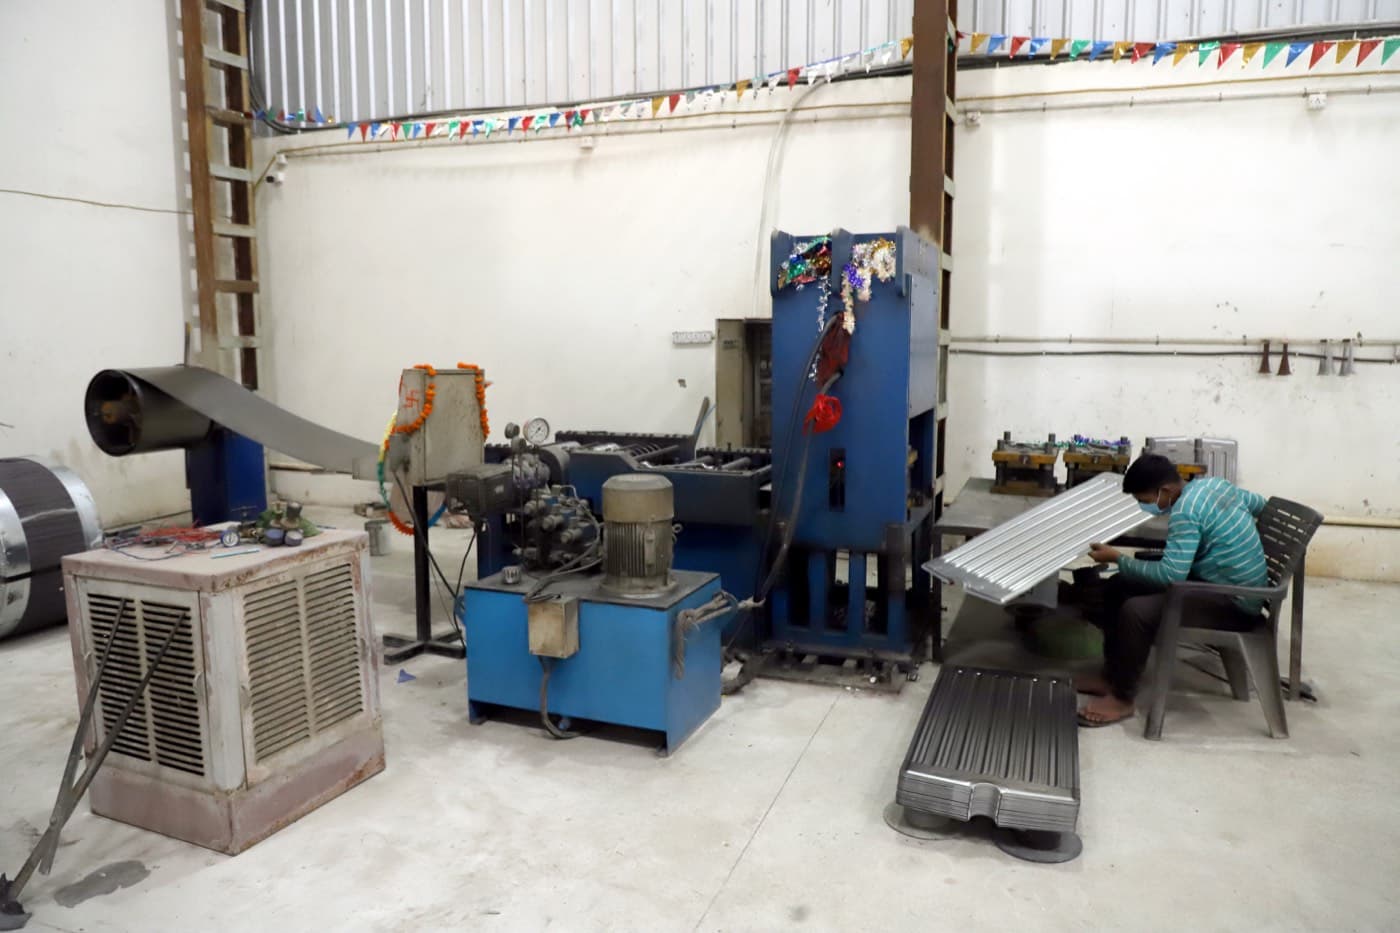
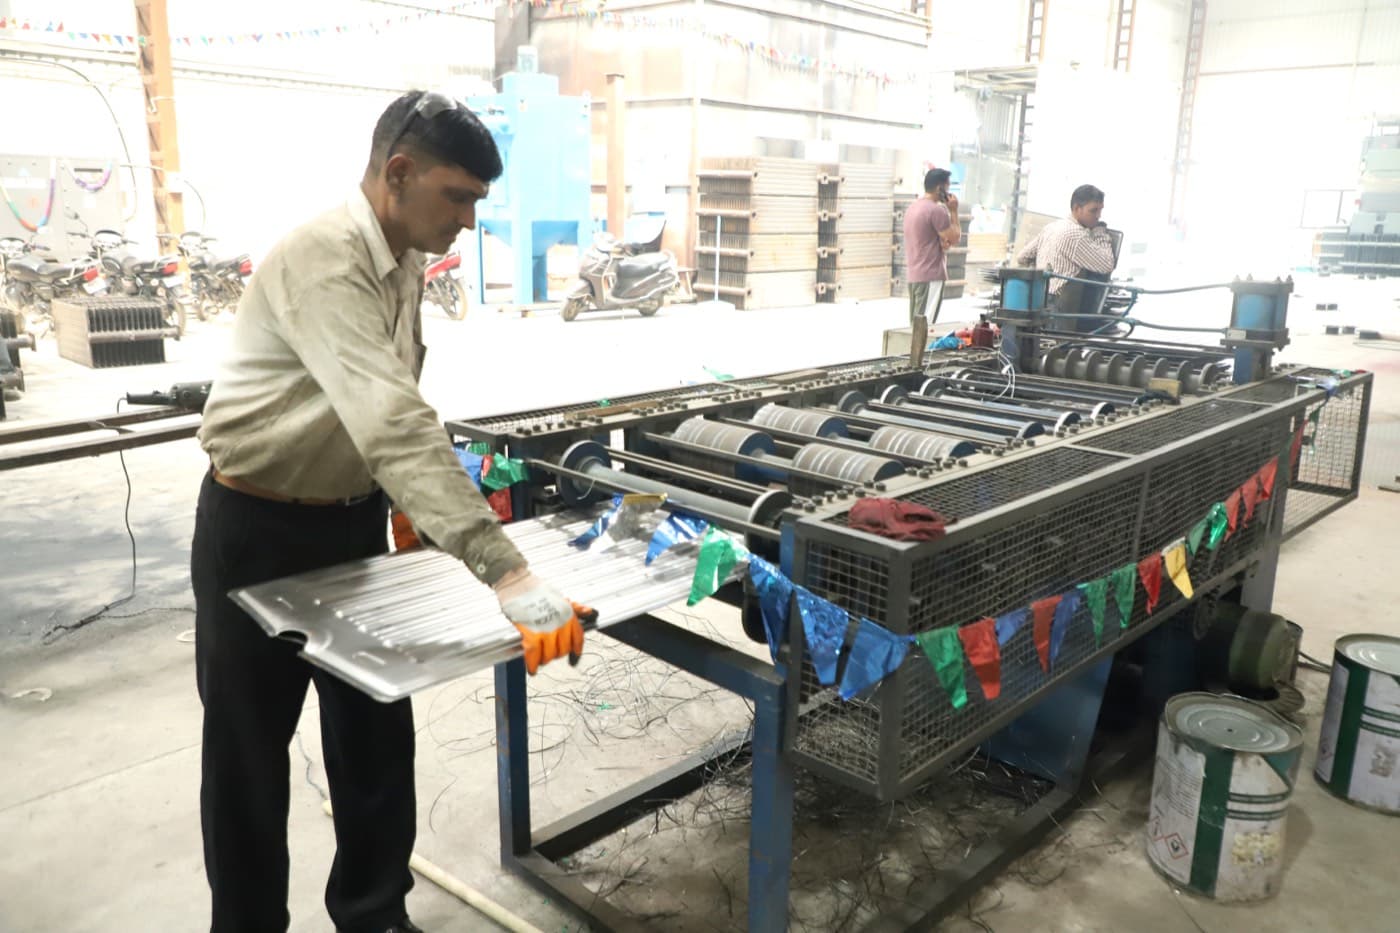
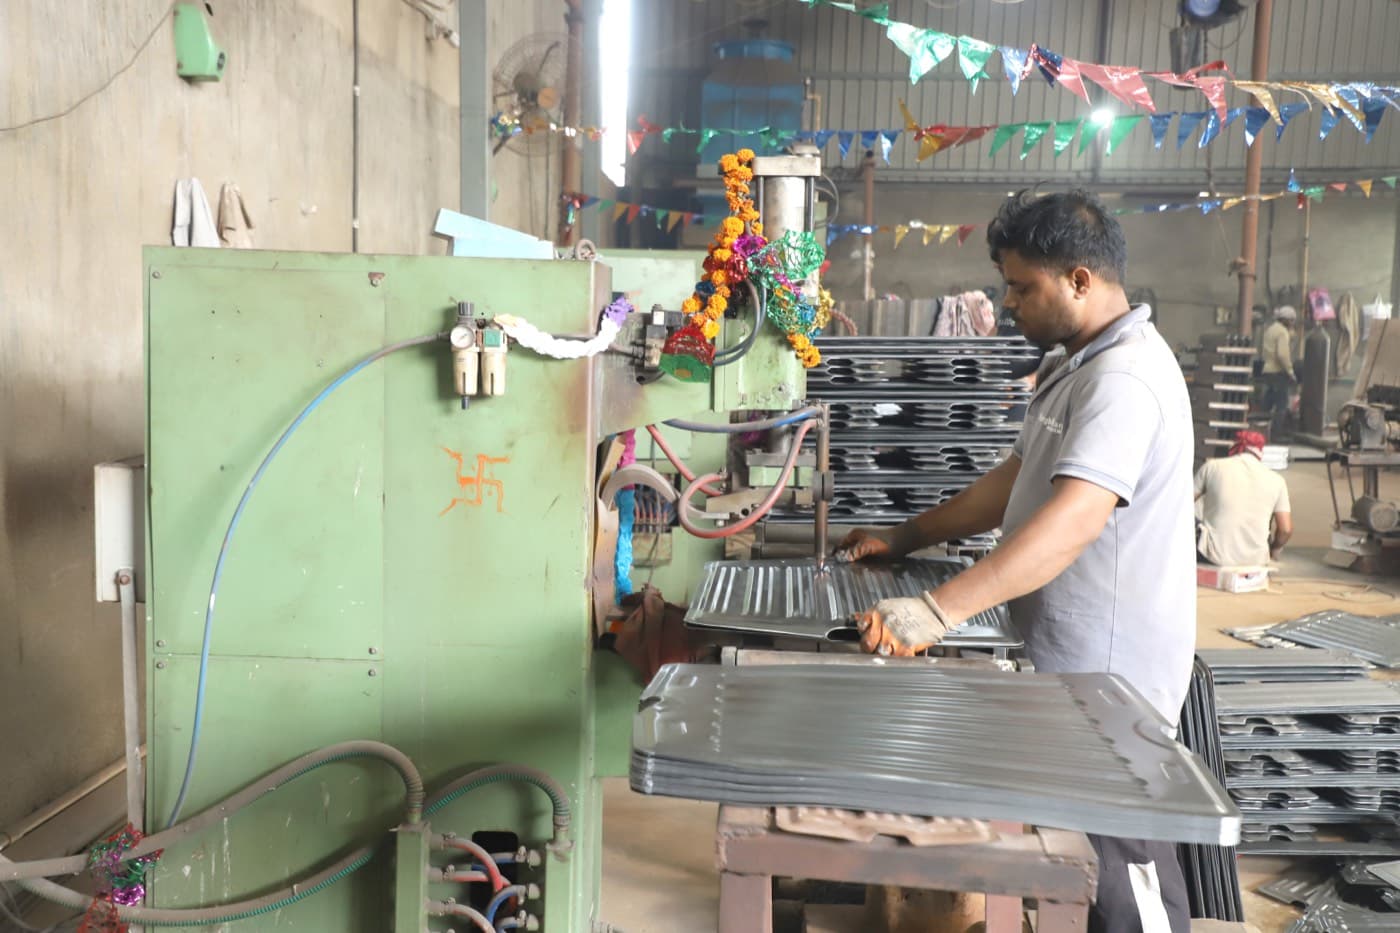
Sheet steel is corrugated and pressed into radiator fins on our roll-forming and spot-seam lines, to 0.8–0.9 mm panel thickness.
- 03
Fabrication
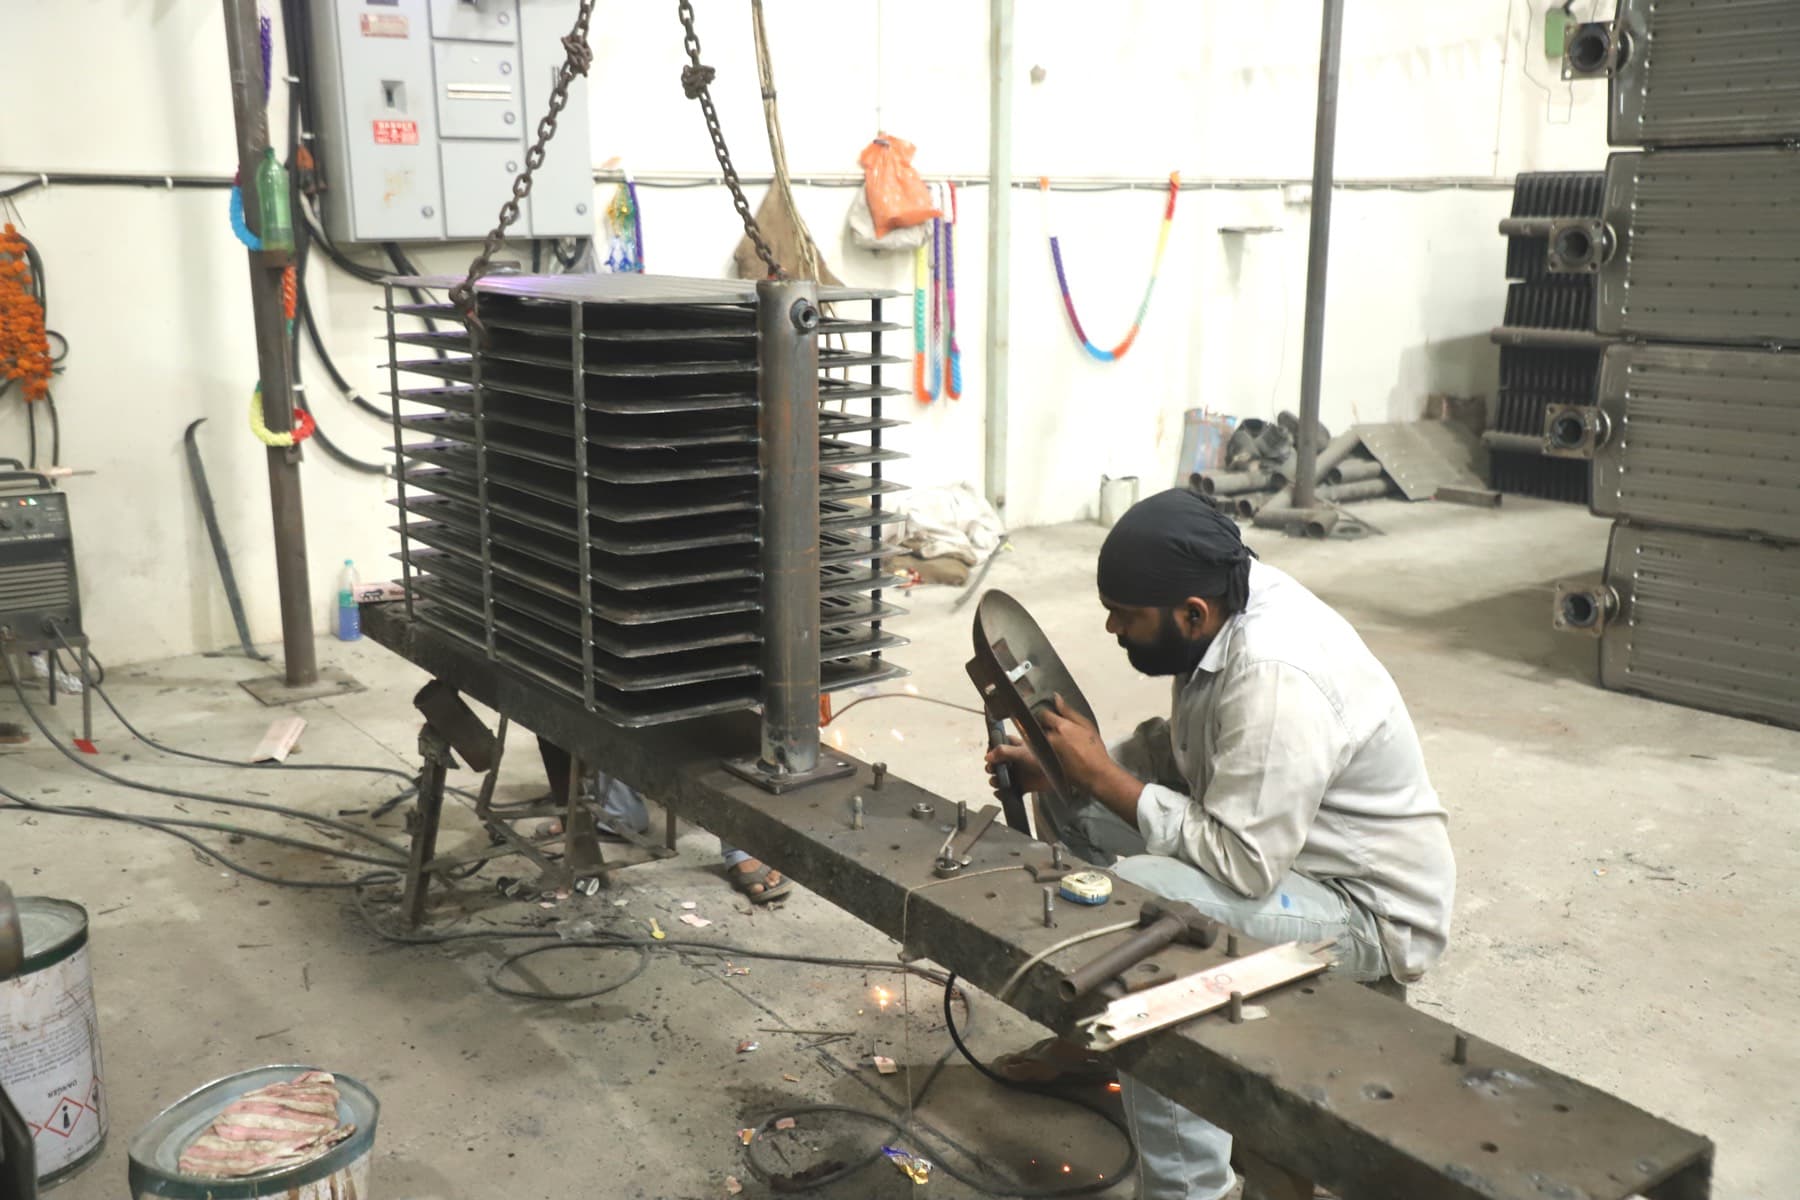
Formed panels are pressed and seam-welded on our spot-seam machine, then trimmed and checked for consistent profile before moving to assembly.
- 04
Welding
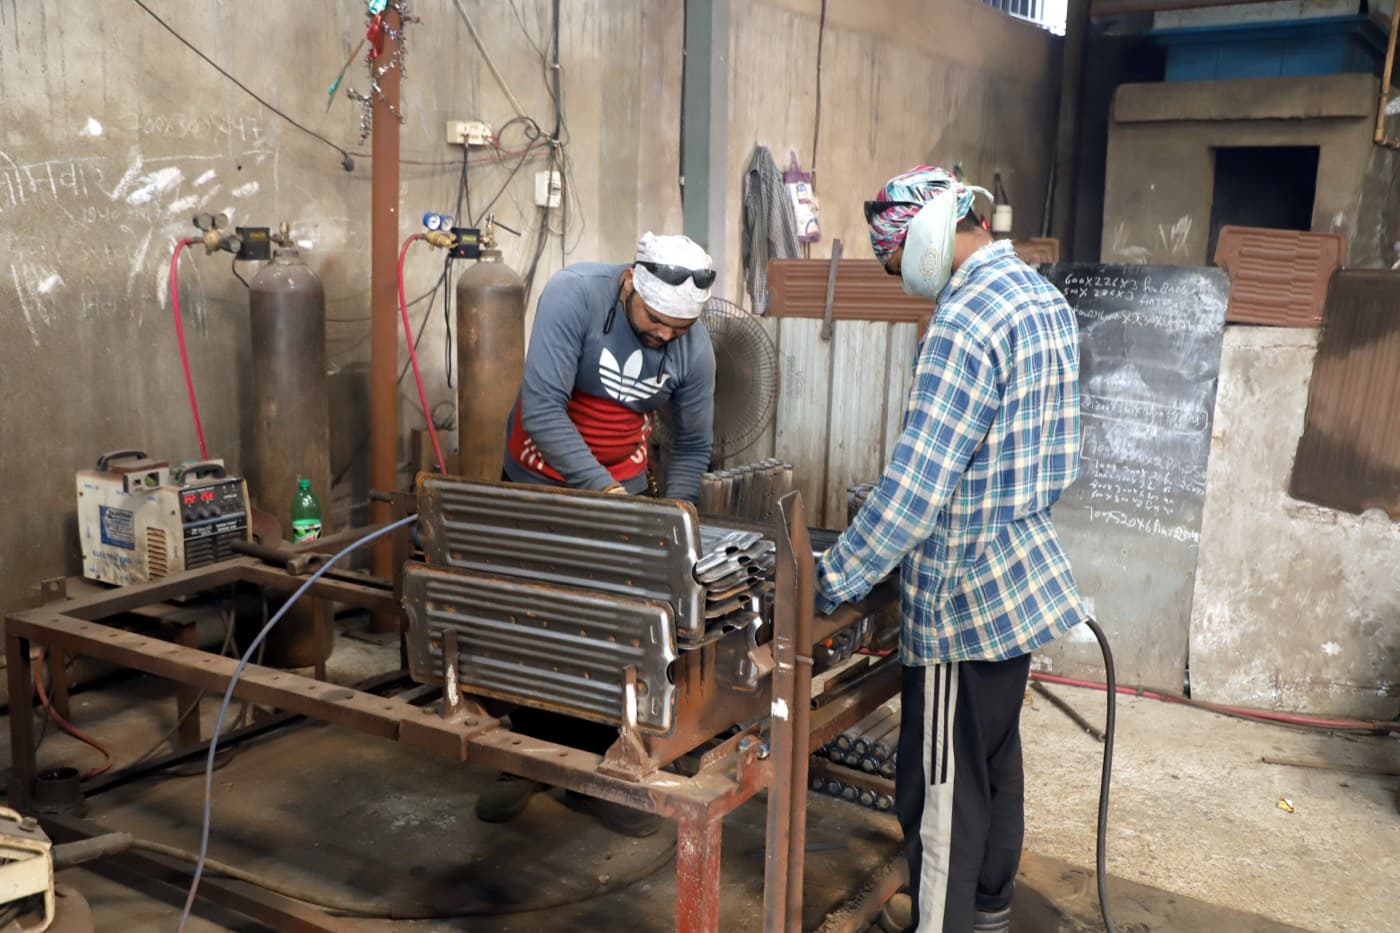
Panels are welded onto mild-steel top and bottom headers to build a complete radiator element, sized to the OD (48/58/75/90 mm) and length called for in the order.
- 05
Assembly
Individual radiator elements are grouped into the finished assembly or bank configuration, with flanges (150 x 150 mm, 12/16/20 mm) fitted per the customer's drawing.
- 06
Inspection
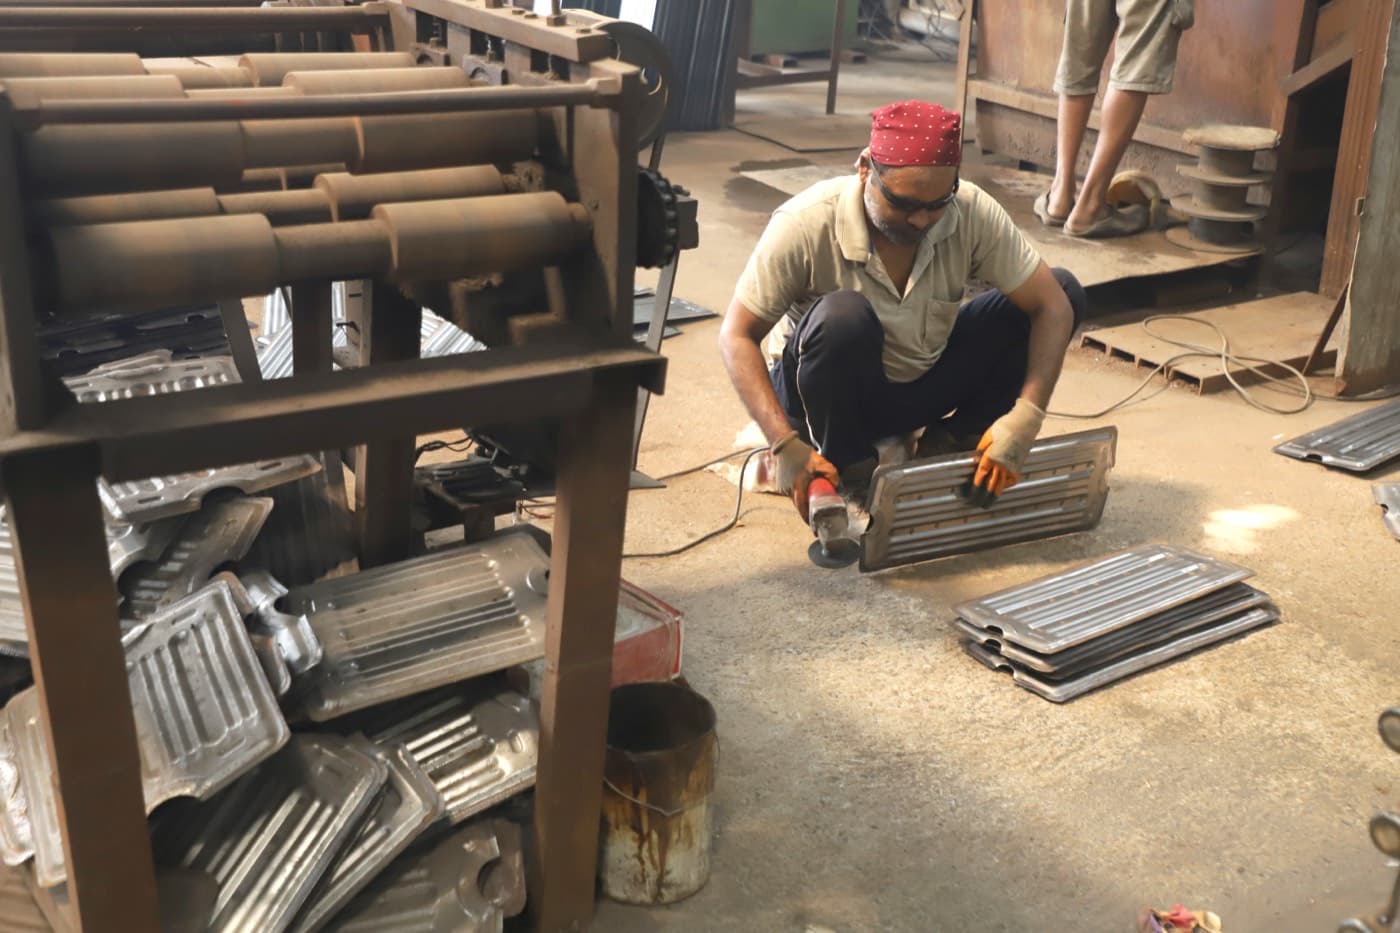
Each assembly is visually and dimensionally checked — panel alignment, weld seams and flange fit — before it goes for testing.
- 07
Testing
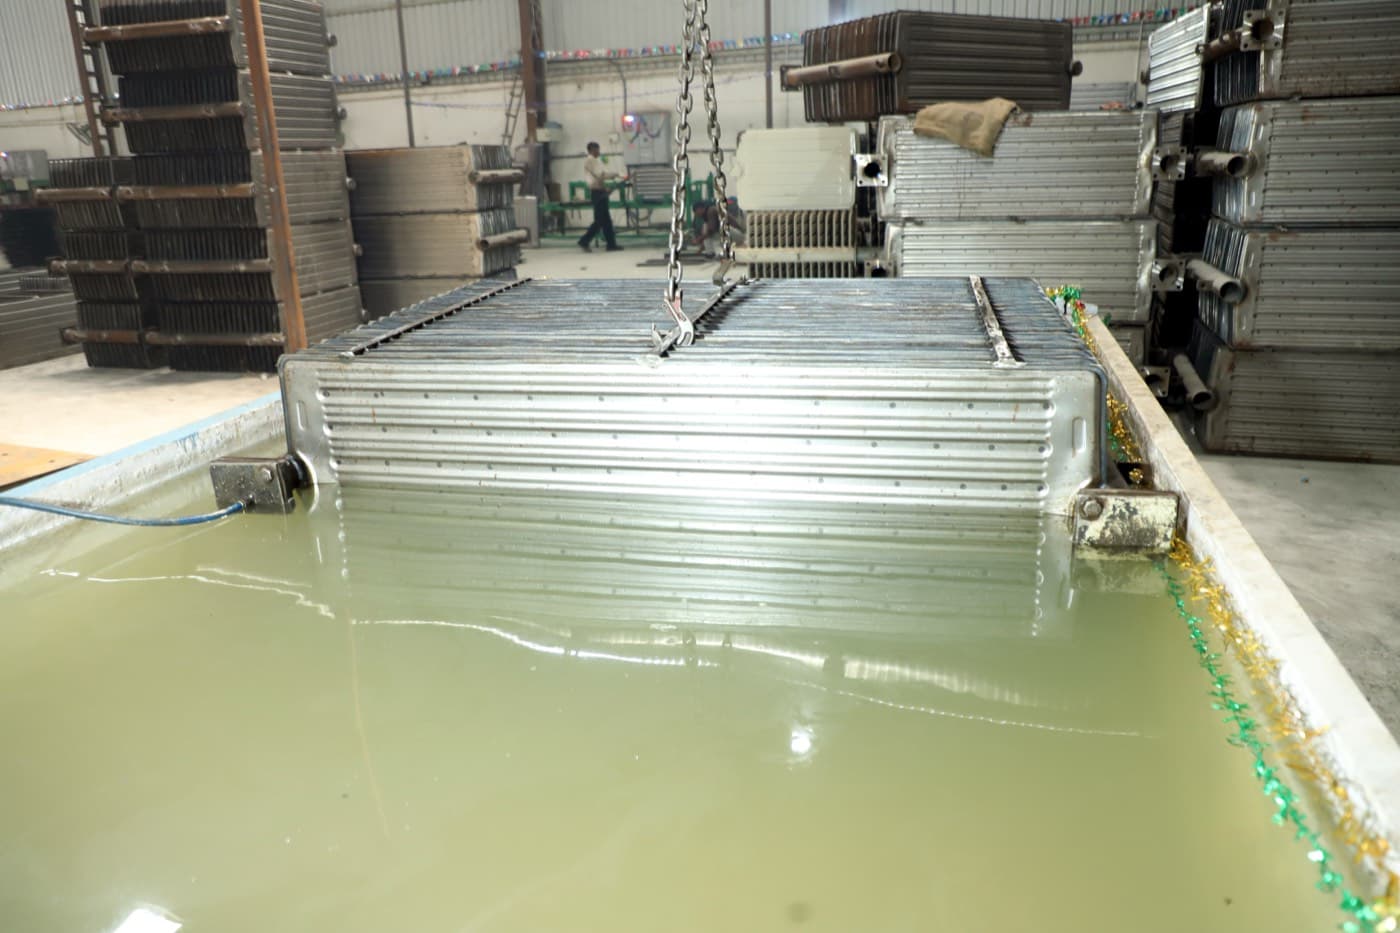
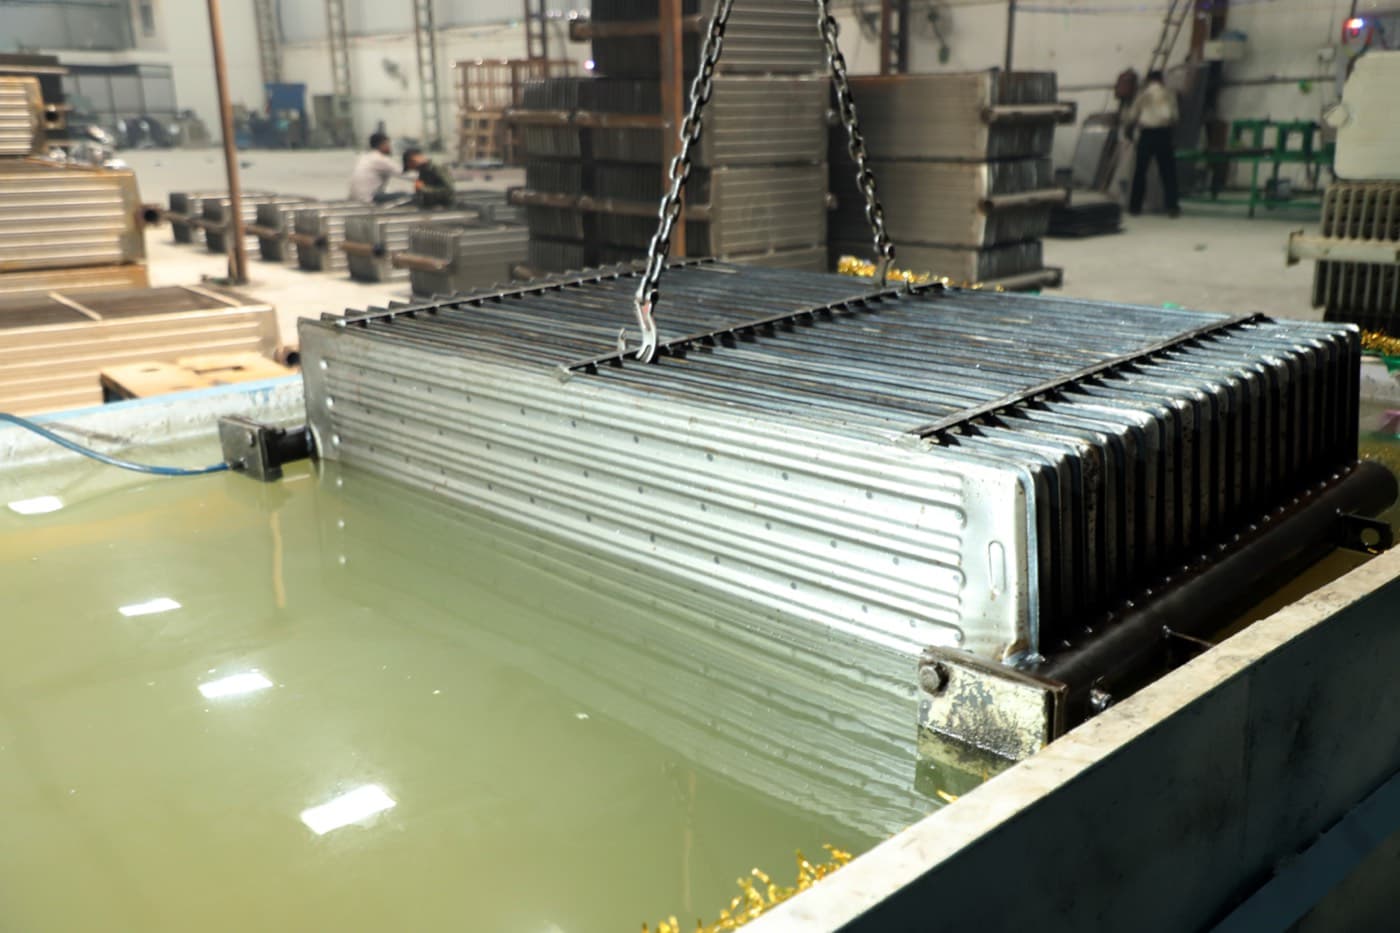
Radiators are submerged and pressure-tested with air and oil at 2.5 kg/cm² — above the 2 kg/cm² maximum operating pressure — to check every weld seam for leaks before it is approved for finishing.
- 08
Finishing
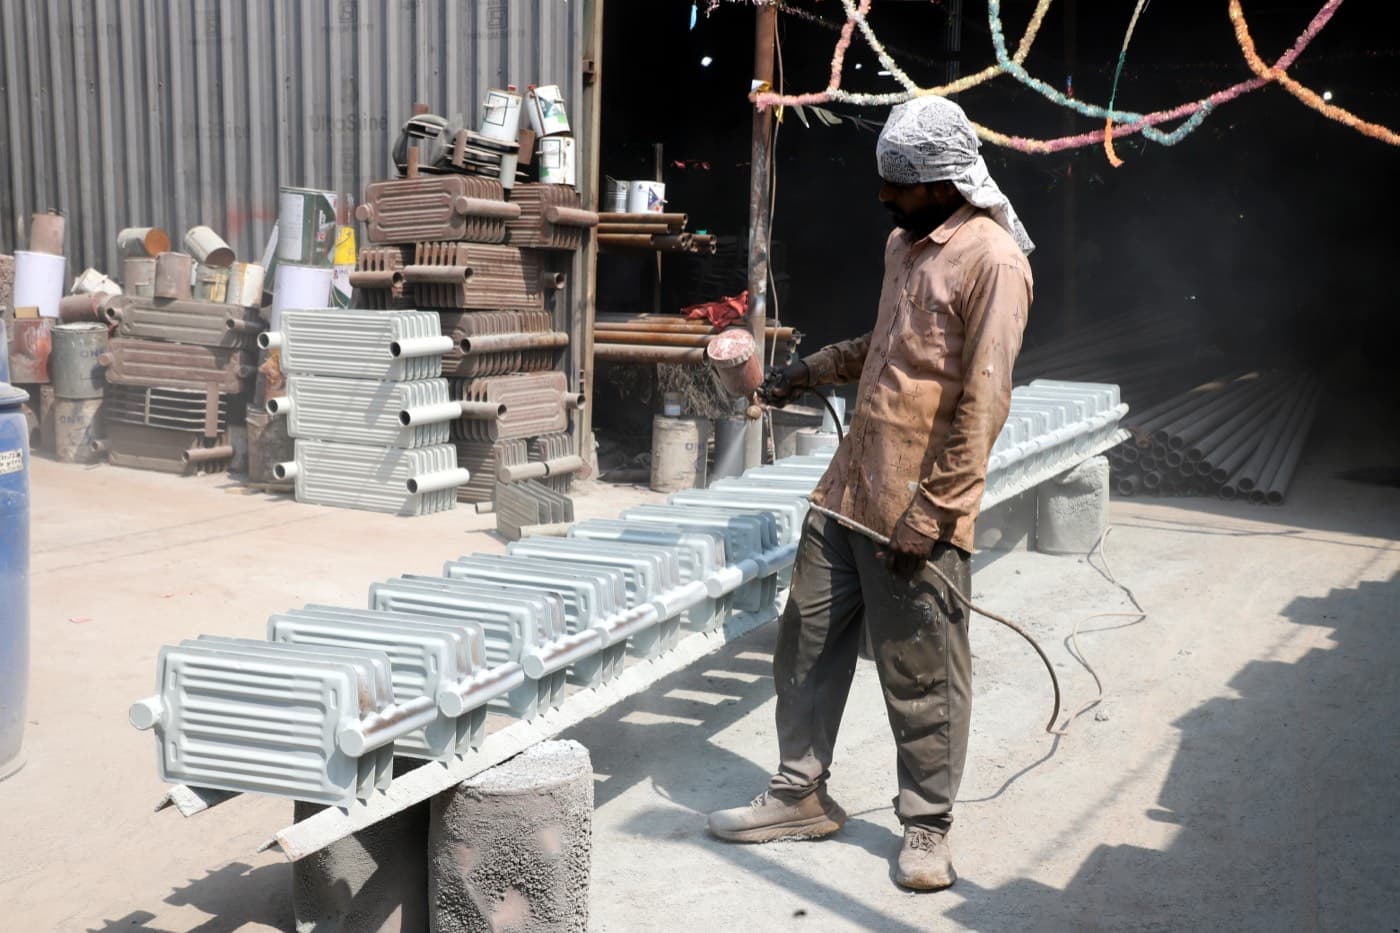
Tested units are surface-prepared and finished with a red-oxide primer followed by a top coat of paint, applied by spray.
- 09
Packaging
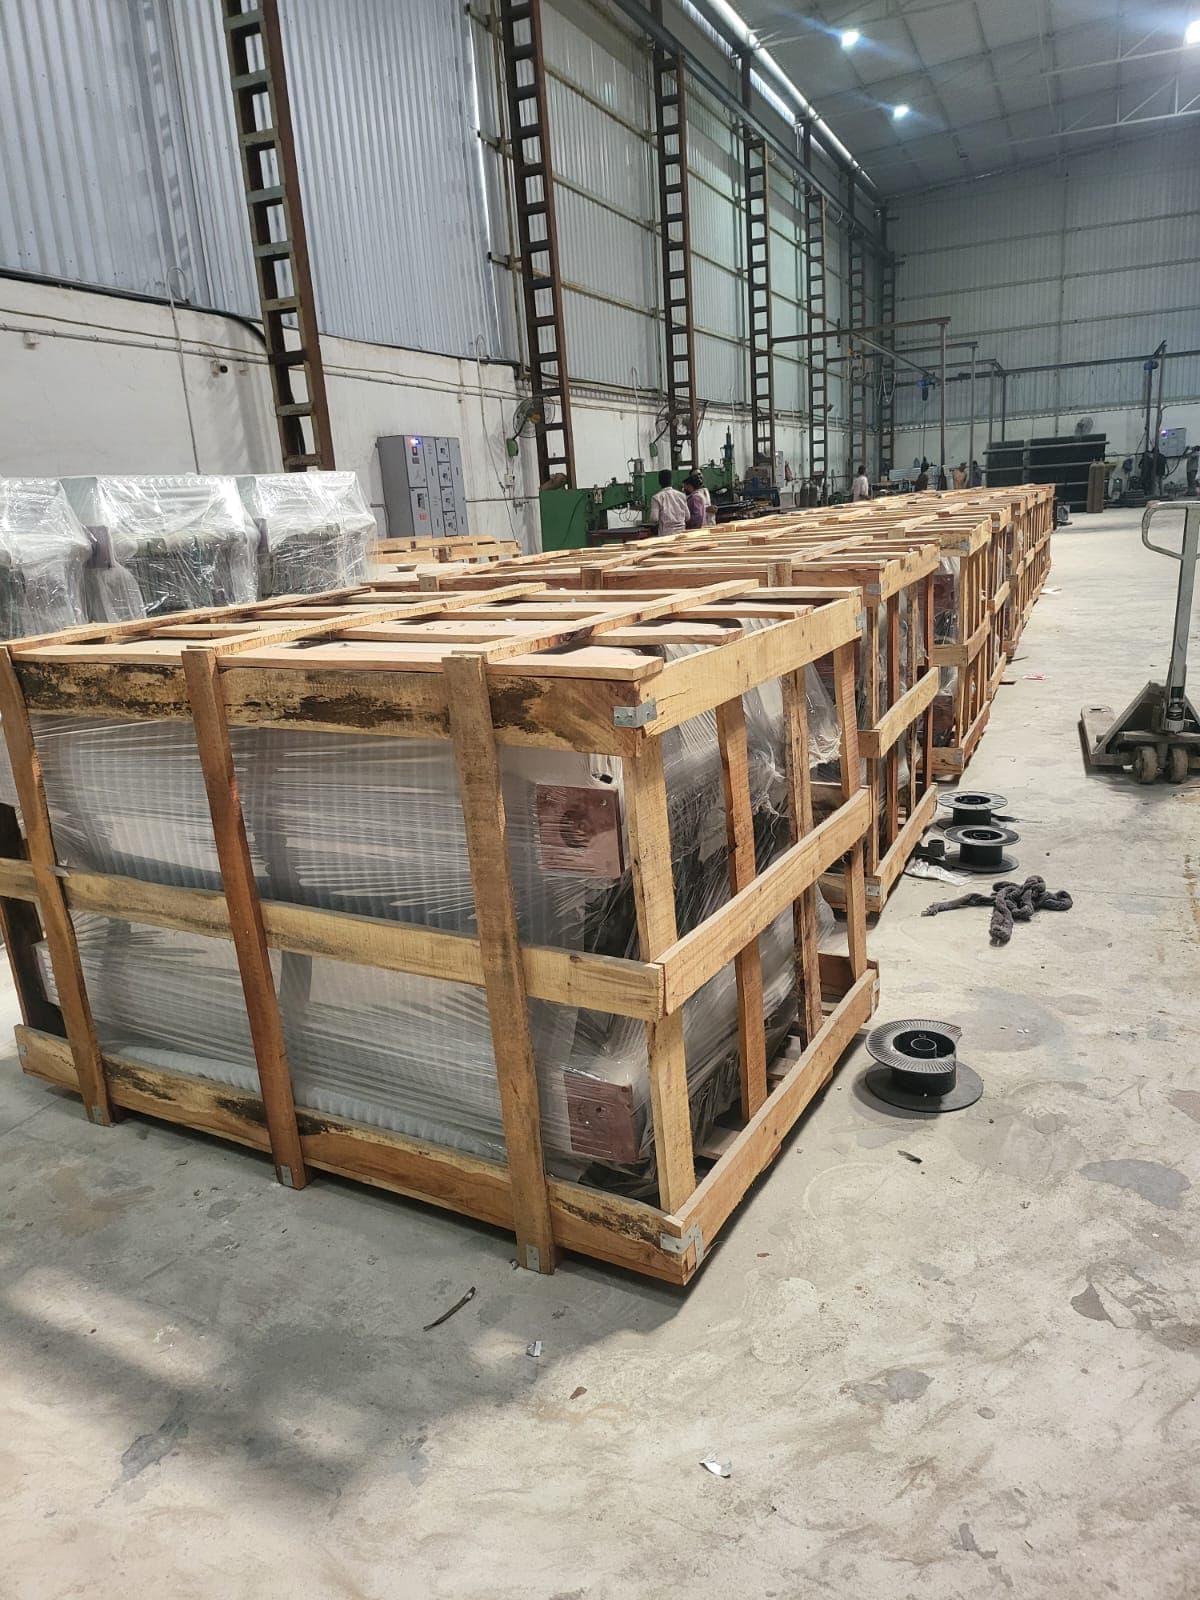
Finished radiators are packed in wooden crates with plastic protective wrapping (packing chargeable separately) ahead of dispatch.
Machinery
Machinery
In-house equipment includes a spot-seam panel welding machine, panel roll-forming/corrugation lines, hydraulic pressing machines, multiple welding stations, a dedicated leak/pressure test tank, and a spray-paint finishing line with dust/fume extraction.
Welding
Welding
Panel-to-header and multi-panel assembly welding is carried out at dedicated welding stations by our fabrication team, with each weld seam checked during assembly and again during pressure testing.
Cutting, Forming & Bending
Cutting, Forming & Bending
Radiator panels are corrugated and formed on roll-forming and spot-seam pressing machines to produce the consistent fin profile used across our 48/58/75/90 mm OD panel range.
Testing
Testing
Every radiator is submerged in our test tank and pressure-tested with air and oil at 2.5 kg/cm² — 25% above the 2 kg/cm² maximum stated operating pressure — before it is cleared for finishing and dispatch.
Surface Treatment
Surface Treatment & Painting
After testing, radiators are spray-finished with a red-oxide primer coat followed by a top coat of paint, applied on our dedicated painting line.
Packaging
Packaging
Finished radiators are packed in wooden boxes with plastic protective wrapping ahead of dispatch. Export/special packing is available and charged separately.
Need Manufacturing Details for Your Project?
Share your drawing or specification and our team will confirm feasibility and lead time.